In the rapidly expanding area of atomic number 3 stamp battery manufacturing, controlling situation conditions is crucial to ensuring production quality and refuge. The sensitiveness of atomic number 3 batteries to moisture requires technical facilities, often referred to as dry suite, where humidity levels are strictly maintained at low thresholds. These environments keep moisture taint during vital manufacturing processes such as electrode preparation, cell meeting place, and promotional material. Consequently, lithium battery dry room equipment and humidness control systems have become necessary components in Bodoni battery production lines, enabling manufacturers to meet demanding timber standards and optimize performance.
The importance of moisture control in atomic number 3 stamp battery production cannot be immoderate. Lithium ions and other sensitive materials used in batteries are extremely absorptive, meaning they pronto absorb moisture from the encompassing air. Even marginal exposure to humidity can degrade the stamp battery s chemical science properties, reduction capacity, life, and refuge. For this reason, manufacturers rely on hi-tech lithium battery dehumidification dry rooms that wield super low relation humidness levels, often below 1. These environments are carefully engineered to provide horse barn, contamination-free atmospheres, minimizing the risk of wet-induced defects or hazards such as short-circuit circuits or energy runaway.
Designing and implementing operational dry suite requires specialised knowledge and equipment plain to the unique needs of atomic number 3 battery production. Standard industrial humidness verify systems are often inadequate for maintaining the ultra-low humidity conditions needful in these environments. This has motivated for usance atomic number 3 stamp battery dry rooms suppliers who volunteer customized solutions that integrate punctilious humidity rule, air filtration, and temperature control. These suppliers work intimately with battery manufacturers to design dry rooms that meet particular product volumes, readiness layouts, and work protocols, ensuring unlined desegregation with present manufacturing processes.
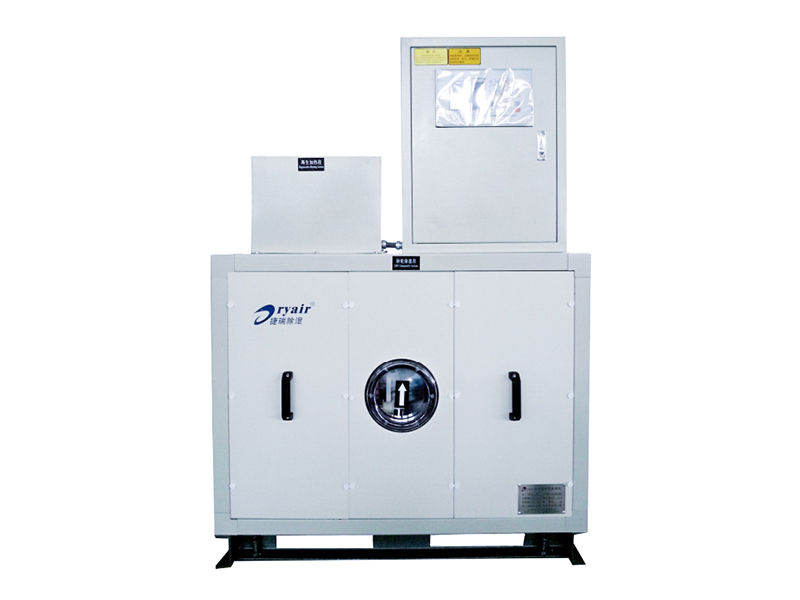
Custom Li stamp battery dry suite typically feature extremely competent dehumidification systems, often based on desiccant engineering, which can remove wet from the air more in effect than traditional refrigeration methods. These systems are subject of maintaining stable humidity levels regardless of external environmental fluctuations, a indispensable factor out in regions with high ambient humidity. Additionally, advanced verify panels and monitoring systems ply real-time data and mechanisation capabilities, allowing operators to fine-tune conditions and chop-chop react to any deviations that could affect production quality.
Beyond dehumidification, the design of these dry rooms also emphasizes air . Particulate contamination can be equally destructive to lithium stamp battery cells, so dry rooms often integrate high-efficiency particulate air(HEPA) filtration to exert cleanroom standards. This ensures that mobile particles do not medium materials or interfere with touchy meeting place processes. The integrating of both moisture and particulate matter control systems creates a restricted that supports the production of high-performance, TRUE Li batteries.
The ontogenesis borrowing of electric car vehicles, inexhaustible vitality store, and portable has led to an exponential function increase in Li battery , which in turn drives design in dry room applied science. Manufacturers now seek custom lithium battery dry rooms suppliers who can provide scalable solutions to play off expanding production lines and evolving industry standards. Flexibility is key, as stamp battery technologies vary in size, interpersonal chemistry, and sensitiveness, necessitating flexible dry room designs. Modular systems that allow for easy expansion or reconfiguration have become particularly pop, sanctioning manufacturers to adjust to market demands without or dearly-won renovations.
Energy efficiency is another critical consideration in the design of lithium stamp battery dry suite. Continuous surgery of dehumidification and air filtration systems can ware substantial world power, so suppliers increasingly focus on on solutions that understate energy use without vulnerable public presentation. Innovations such as heat retrieval systems, sophisticated control algorithms, and high-efficiency components help reduce work costs and environmental affect, orienting with sustainability goals embraced by many battery manufacturers.
Moreover, safety remains a top priority in environments handling lithium stamp battery materials. Custom dry room designs incorporate features to palliate fire and plosion risks, including non-sparking materials, appropriate ventilating system, and reply systems. Compliance with international safety standards and regulations is mandate, and skilled suppliers assure that their equipment and facilities meet all necessary certifications, providing peace of mind aboard operational .
In sum-up, lithium battery dry room equipment and humidity verify systems form the spine of tone self-confidence in Li stamp battery manufacturing. The delicate nature of battery components demands environments with incisively limited low humidity and clean air, achievable only through technical, usance-engineered dry suite. As the manufacture grows and technologies germinate, the role of usance Li stamp battery dry rooms suppliers becomes progressively vital, delivering tailored solutions that balance demanding environmental requirements, operational flexibility, vitality , and refuge. For manufacturers aiming to make honest, high-performance Li batteries, investment in hi-tech dry room infrastructure is a plan of action jussive mood that supports both invention and long-term achiever.
